En (UK)
 De
 zh-CN
 Se
 En (US)
 Nl
 Fr

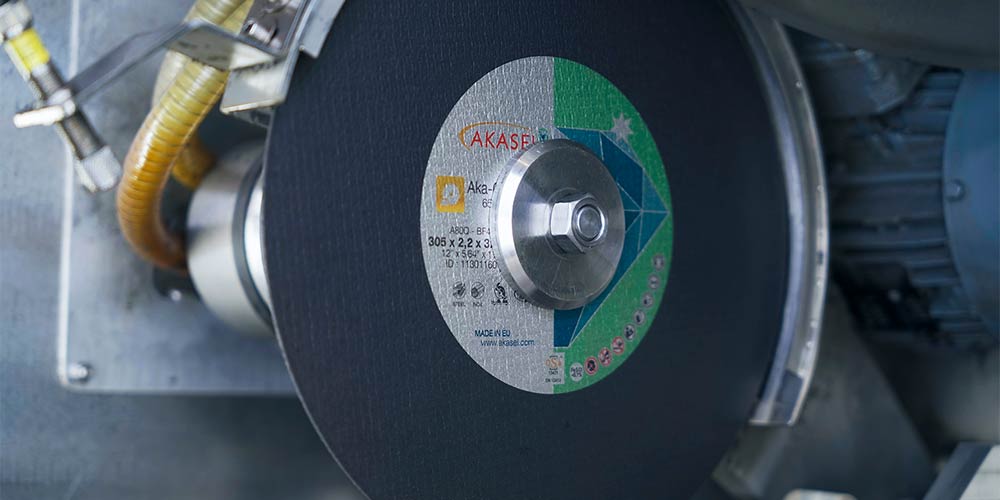
The Aka-Cut 350 HV, Aka-Cut 500 HV and Aka-Cut 650 HV are high-performing reinforced cut-off wheels perfect for routine cutting. Each wheel is specifically designed for a particular hardness range. The Akasel Aka-Cut reinforced wheels contain aluminium oxide (Al2O3) as an abrasive grain. This makes the cut-off wheel hard and durable, providing excellent cutting results.
Durability and stiffness are the result of a fibre web built into both sides of the wheel. These cut-off wheels are developed and optimised to help you achieve the best cutting result.
We have optimised the diameter of the fibre web filament used, to promote optimal cooling and lubrication at the cutting surface. The fibre web produces a three-dimensional effect aiding in the channelling of coolant to the cutting edge.
The fibre reinforcement provides maximum durability and stiffness. It also makes the wheel better to withstand internal stress and tension when cutting surface hardened materials. This means that the risk of breaking the wheel is low, especially in cases where hardened samples are cut. High residual tension in the sample, in some cases, can “clamp” the cut-off wheel, resulting in sudden failure. The risk of catastrophic failure can be reduced when using the Aka-Cut reinforced wheels, as a result of the reduced surface area and friction from the web surface.
The optimised grain size of the abrasives used in the wheel produce a high quality surface finish, equivalent to the surface produced when grinding with a Rhaco Grit P320. This surface finish will reduce the time required for subsequent grinding and polishing steps and may even remove an initial grinding step in some cases.
The Aka-Cut reinforced cut-off wheels are characterised by:
- High surface quality
- Lower breakage risk
- Cost efficiency
Technical Information and Insights
Aka-Cut 650 HV can be used for cutting all types of harder steel, and is especially suited for hardened samples with a hardness of 500-700 HV. This is an Al2O3 cut-off wheel with resin bond.
Aka-Cut 500 HV can be used for cutting all types of medium hard steel, and is especially suited for hardened samples with a hardness of 250-500 HV. Aka-Cut 500 HV is an Al2O3 cut-off wheel with resin bond.
Aka-Cut 350 HV can be used for cutting all types of softer steel, and is especially suited for ferrous samples with a hardness of 200-350 HV. This is a resin bonded Al2O3 cut-off wheel.
Technical Information and Insights
Wearability and Surface Finish
| Value | Aka-Cut 650 HV | Aka-Cut 500 HV | Aka-Cut 350 HV |
| Material | Hardened tool steel 100MnCrW4 680 HV | Tool steel X40CrMoV51 450 HV | 0.45% C steel Normalised 180 HV |
| Q | 4–6 | 4–6 | 4–6 |
| Ra | 0.2–0.3 µm | 0.2–0.3 µm | 0.2–0.3 µm |
| Parameters for testing |
| Cutting feed: 0.5 mm/s |
| Material diameter: 40 mm |
| Periferical speed: 43 m/s |
“Q-value” is a measure of a cut-off wheel’s wearability. A Q-value of 4 means the wheel can make four times as many cuts as a wheel with a Q-value of 1.
When using a cut-off wheel with a Q-value of 1, the wheel’s wear is equivalent to the material that has been cut. For example, ø40mm is equivalent to 2.5 mm wheel wear on a new 305 mm wheel. Or in the case of these Aka-Cut wheels with a Q-value of 5, about 0.5 mm.
“Ra-value” refers to surface roughness, specifically average roughness (Arithmetic Average Roughness). An Ra-value of 0.2-0.3 μm is approximately equivalent to the surface produced when using Rhaco Grit P320 on 0.45% C steel for 60 seconds.
Other Technical Information
- Diameter (⌀): 254 mm to 406 mm
- Arbour hole diameter (⌀): 32 mm
- Thickness:
| Wheel Diameter (⌀) | Thickness |
| 254 mm | 1.7 mm |
| 305 mm | 2.2 mm |
| 356 mm | 2.6 mm |
| 406 mm | 3.2 mm |
- Grain type: Aluminium Oxide (Al2O3)
- Grain size: P80
- Binder: Phenolic
- Full side reinforcement 2.2 mm 2.6 mm 3.2 mm
- Forwetcutting, recommended to be used in conjunction with Aka-Cool
- Recommended rpm:
| Wheel Diameter (⌀) | Akasel Aka-Cut Reinforced Wheels (RPM) |
| 254 m | 3300 rpm |
| 305 mm | 2750 rpm |
| 356 mm | 2350 rpm |
| 406 mm | 2050 rpm |
If higher speeds are used, the wheel will act as if it is harder. That means wear less and with possible burns. Equally when a lower rpm is used, the wheel will act softer which means higher wear, but lower chance of burning.
- Feed speed: suggested 0.5 mm/s. For metallographic sectioning, feed-speed varies between 0.25 mm/s and 2.0 mm/s. Refer to the machine manufacturer’s manual and operating instructions.
- The arbour hole is reinforced with a metallic flange, to increase the strength of the wheel, but also to prevent damage and unnecessary wear to the cut-off machine.
Who Should Use Reinforced Cut-off Wheels?
Aka-Cut reinforced wheels are to be used in industrial, busy facilities, where a robust wheel is required. Our cut-off wheels cover a variety of materials due to different bond systems. The cut-off wheels are optimal to use for:
- Production, metallurgical, quality control and assurance laboratories or similar, where the following are required:
- Perfect for wet abrasive cut-off machines with manual operation
- Forfast cutting procedures
- Forcastings
- Fortempered steel
- Formild or annealed steel
- Forlowcarbon steel
- Forstainless steel
- Forgeometry-related parts
- Steel makers
- Automotive component manufacturers
Recommendations to Obtain the Best Sectioning Results
- Always ensure the specimen is clamped correctly, it must not move during the cutting process.
- Always ensure the specimen is positioned in such a way to reduce the section of material that must be cut.
- Always ensure that there is fresh coolant being applied during the cutting process. Use a suitable additive, which provides cooling, lubrication and acts as a corrosion inhibitor.
- Aka-Cool is free from amine and boric acid and therefore has an extremely low allergy potential.
- The dilution ratio for preparing Aka-Cool with water is 3-5% for optimal performance.
Note: Aka-Cool is a water-based additive and therefore it is necessary to leave the door of the cutting chamber open after the cutting process, to allow for water to evaporate, leaving a protective coating on the surfaces inside the cutting chamber of the cut-off machine.
- There should not be excessive foam during the cutting process. Should this occur, the cooling will not be optimal and damage to the specimen is most likely. Use Aka-NoFoam to avoid excessive foaming. If it is necessary to replace the coolant refer to the manufacturer’s manual and operating instructions. And follow local legislation regarding the disposal of the used coolant mixture.
- Aka-NoFoam is mixed with water at a concentration of 0.5-1.0%.
- Always ensure that the correct type of cut-off wheel has been selected for the material. Akasel has a complete range of cut-off wheels offering a comprehensive solution for all cutting applications:
- Premium cut-off wheels
- Reinforced cut-off wheels
- Precision cut-off wheels
- Superabrasive cut-off wheels
- Always ensure that the recirculating unit is clean and if too much sediment is built up the cooling system, filter bags, etc. should be replaced. Refer to the manufacturer’s manual and operating instructions.